


Cleaning and Sanitation
Your breast milk never shares our equipment with anyone else's. We process one mom's milk at a time — and between every batch, every surface and every piece of equipment is thoroughly cleaned, sanitized, and disinfected. What goes in as yours comes out as yours.

Food Safety Credentials
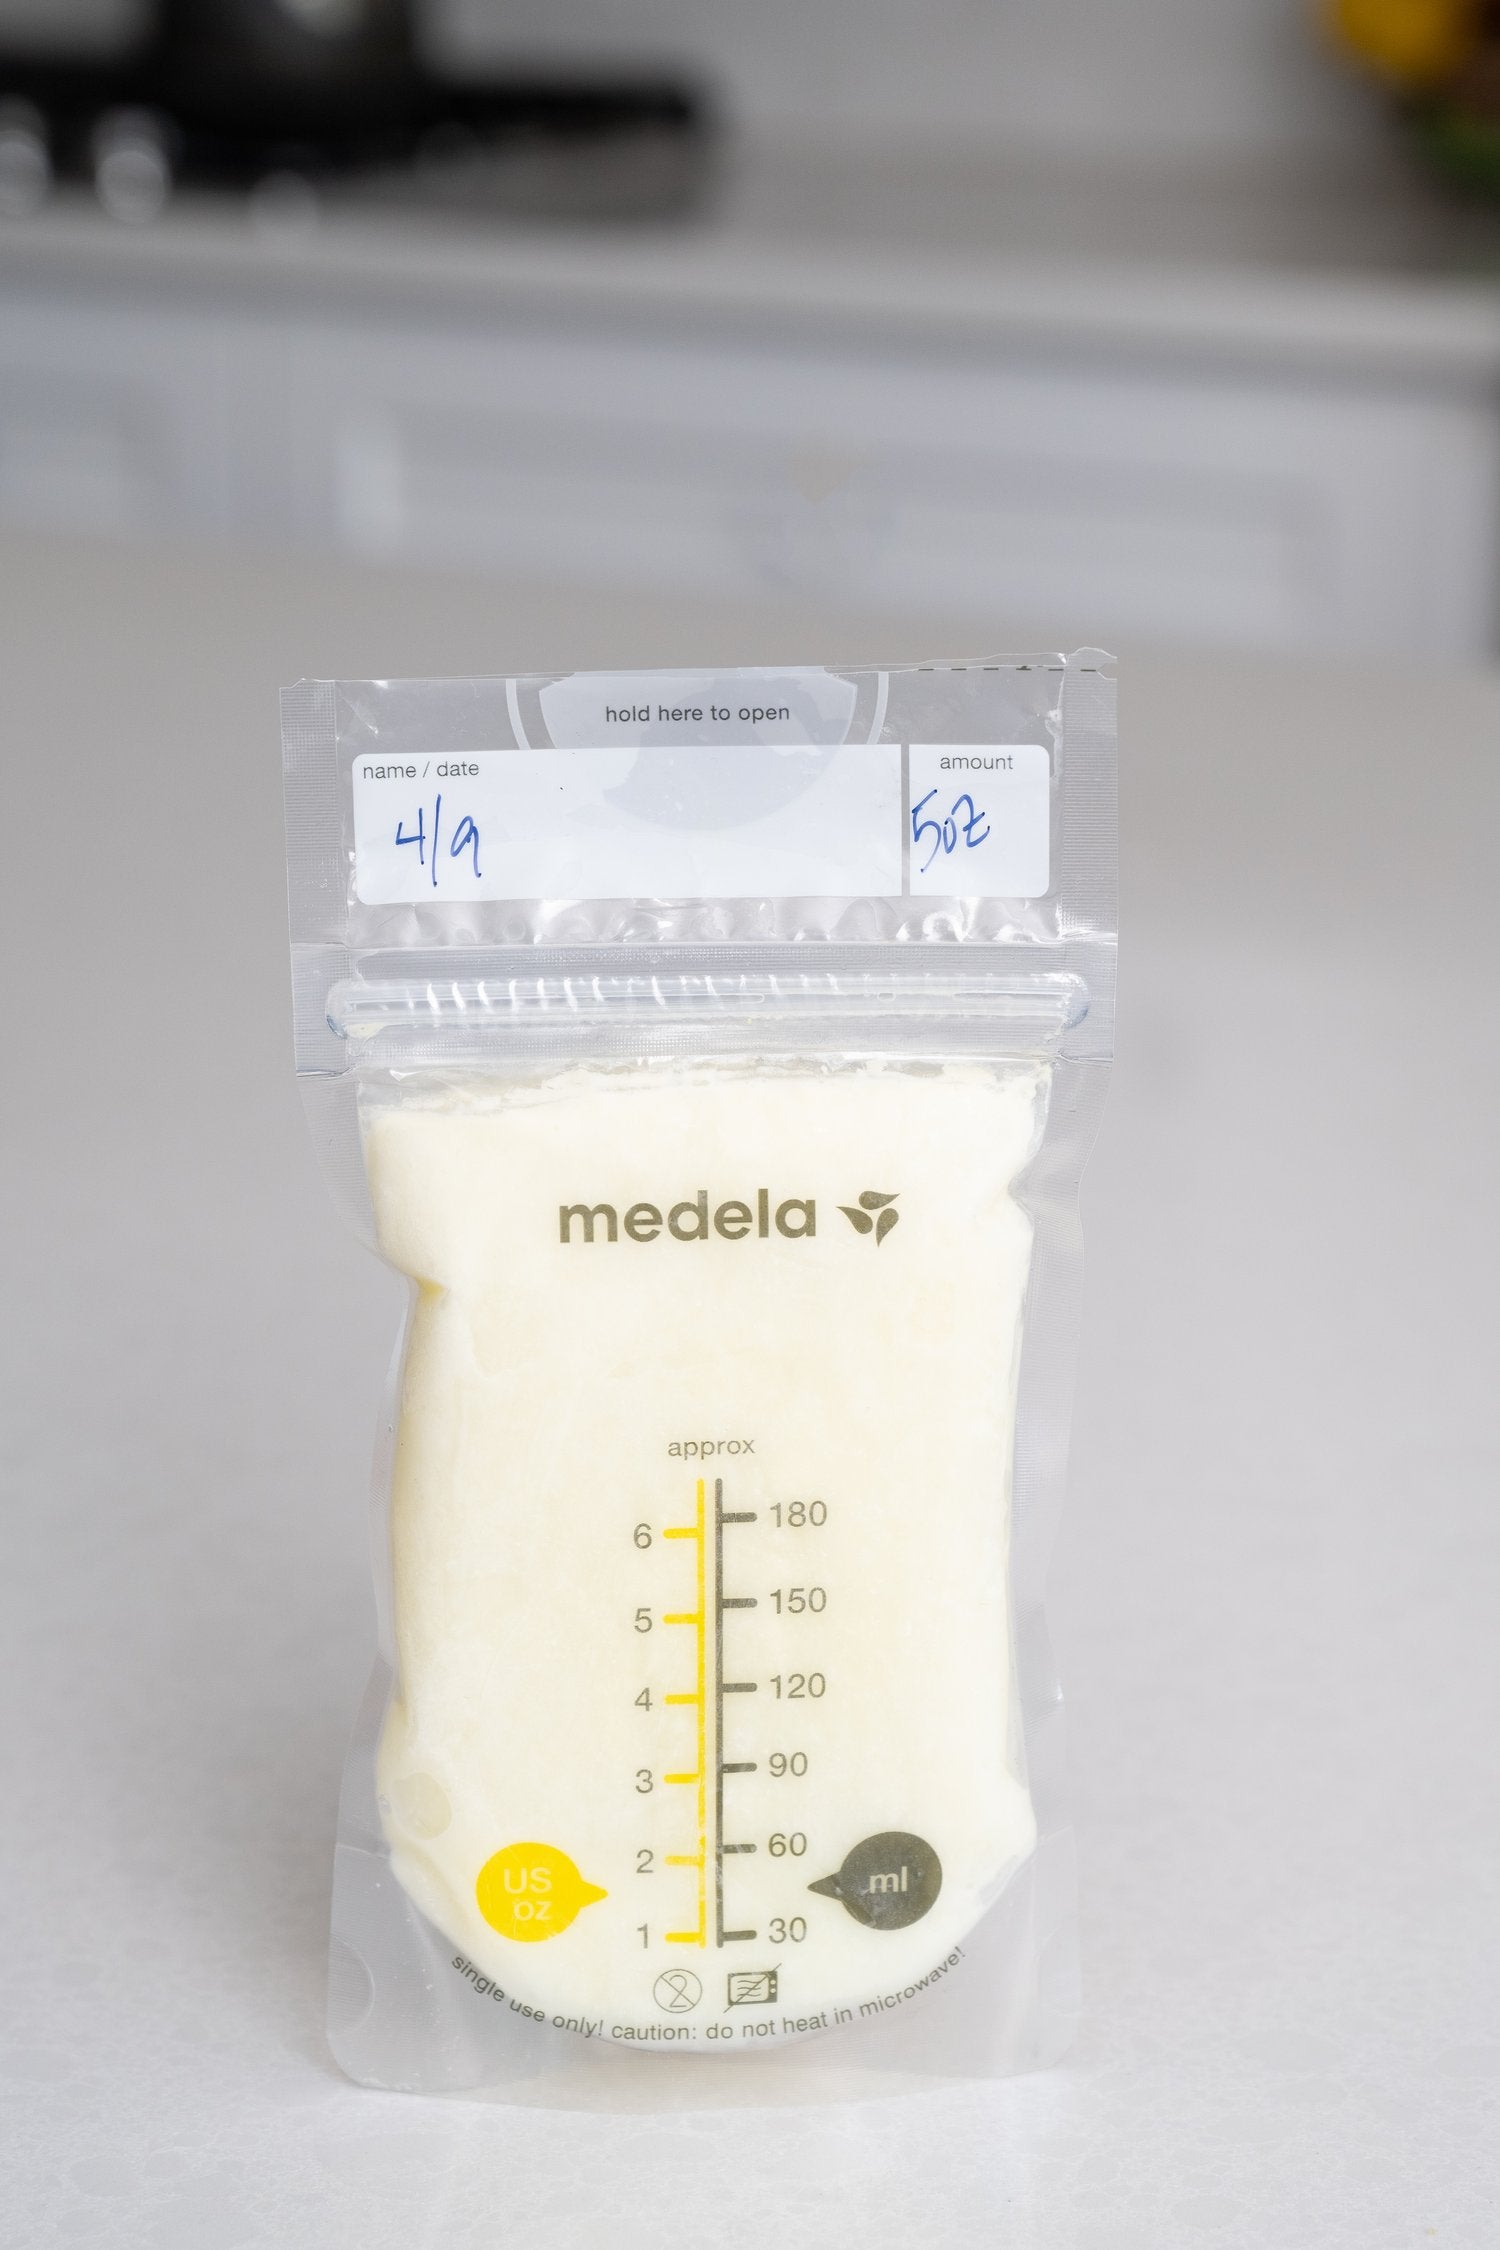
Our entire team is food safety handler and aseptic technique certified — because the people handling your milk should be trained to the same standard as any medically-sensitive food environment. The moment your cooler arrives, we inspect, document, and label your milk individually, then store it in a dedicated labeled bin until it's ready to process.

Sterile Handling
During packaging, your breast milk powder never enters open air. Our facility uses an ISO 5 laminar flow hood, a medical-grade clean air environmen, to ensure nothing is introduced during the packaging step. Your finished pouches are sealed in high-barrier mylar bags that protect against moisture, oxygen, UV light, and contamination.

Temperature Control Monitoring
From the moment your cooler arrives, we log your breast milk's temperature. Your milk stays in a dedicated, remotely monitored freezer — so we know it's staying frozen even when no one is physically in the building. And if the power goes out? Our freezers and freeze dryers run on backup generators. Milk by Mom stashes don't depend on the grid.

Quality Control Testing
Every batch is tested before it leaves our facility. We conduct water activity checks using laboratory-grade equipment, the same standard used in pharmaceutical and food safety environments, to confirm your freeze-dried milk will remain shelf-stable for up to three years without refrigeration. You don't get your pouches until we're certain they pass.

Environmental Testing
We don't just clean — we verify. Our processing rooms and equipment are regularly tested to confirm our sanitization practices are working. We routinely test for total aerobic plate counts, E. coli, yeast, mold, Listeria monocytogenes, Bacillus cereus, Staphylococcus aureus, and Cronobacter sakazakii. If something is present, we catch it before it's ever near your milk.

Medical-Grade Shipping
Your breast milk doesn't just travel safely inside our facility — it travels safely to get here. We ship via UPS Healthcare, the same carrier trusted for transporting biological and temperature-sensitive materials. Your cooler is tracked from the moment it leaves your door to the moment it arrives at ours.


